
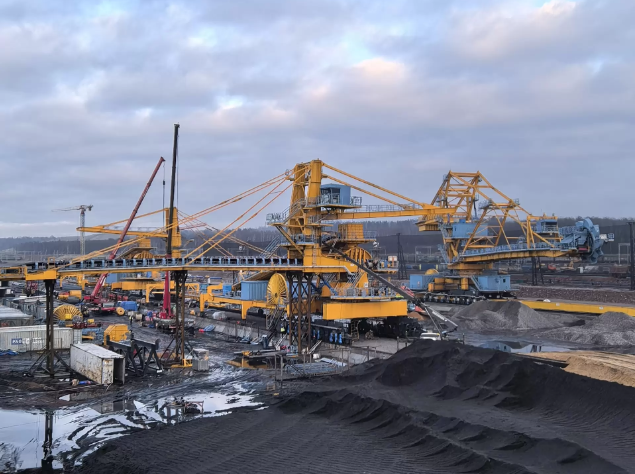
Bucket Wheel Stacker Reclaimer: A Complete Guide to Bulk Material Handling
A bucket wheel stacker reclaimer is an essential piece of equipment for large-scale bulk material handling.
A bucket wheel stacker reclaimer is an essential piece of equipment for large-scale bulk material handling. By combining stacking and reclaiming functions in one integrated machine, it helps industrial facilities manage stockpiles efficiently and maintain a continuous flow of materials. It is widely used in steel plants, power stations, mining operations, cement plants, ports, and other industries that handle large volumes of bulk materials.
Materials such as iron ore, coal, limestone, pellets, and coke require reliable storage and transportation systems. A well-designed bucket wheel stacker reclaimer can improve stockyard organization, support consistent material supply, and reduce the need for separate machines for stacking and reclaiming.
What Is a Bucket Wheel Stacker Reclaimer?
A bucket wheel stacker reclaimer is typically a rail-mounted machine consisting of a bucket wheel, boom conveyor, traveling mechanism, slewing mechanism, luffing system, and electrical control equipment.
During stacking, the machine receives material from an incoming conveyor and distributes it across the stockyard to form stockpiles. During reclaiming, the rotating bucket wheel collects material from the stockpile and transfers it onto a conveyor system for delivery to downstream facilities.
This combined design makes the equipment particularly suitable for large stockyards where materials must be stored, recovered, and transported according to production requirements.
How Does It Work?
The machine operates through coordinated mechanical movements and conveyor transportation. The bucket wheel rotates continuously, collecting material from the stockpile and transferring it to the boom conveyor. The material then moves onto downstream conveyors for further processing or transportation.
The traveling mechanism allows the machine to move along stockyard rails, while slewing adjusts the horizontal working direction and luffing changes the boom's vertical angle. Together, these movements enable the bucket wheel to reach different areas of a stockpile.
During stacking, the material flow follows the opposite route, moving through the conveying system and discharging from the boom to build the stockpile. Coordinating these operations with the wider conveyor network helps maintain efficient material flow throughout the stockyard.
Main Components of a Bucket Wheel Stacker Reclaimer
Several key components work together to ensure stable and reliable operation.
Bucket Wheel: The bucket wheel is the main reclaiming component. Multiple buckets mounted around a rotating wheel collect material from the stockpile. Its design must account for material density, particle size, abrasiveness, required capacity, and wear resistance.
Boom Conveyor: The boom conveyor transfers material between the bucket wheel and the machine's transfer point. Belt alignment, drive selection, tension control, and conveyor capacity are important factors in maintaining continuous operation.
Traveling Mechanism: This system moves the entire machine along the stockyard rails. Drive units, wheels, gearboxes, and braking components must work together to provide stable movement and accurate positioning.
Slewing and Luffing Mechanisms: Slewing controls horizontal movement, while luffing adjusts the boom angle. These mechanisms allow the machine to accommodate different stockpile heights, widths, and operating positions.
Electrical and Control System: The control system coordinates machine movements, conveyor operation, safety interlocks, and monitoring functions. Modern equipment can incorporate PLC controls, positioning sensors, and automation technologies to improve operational accuracy.
Common Applications Across Industries
Bucket wheel stacker reclaimers are used wherever large quantities of bulk materials need to be stored and recovered efficiently.
In steel plants, they handle iron ore, coal, pellets, coke, limestone, and other raw materials required for production. In power stations, they support coal stockpiling and fuel supply systems. Mining operations use them to manage ore and mineral stockpiles, while ports and terminals rely on them to transfer bulk materials between storage yards and transportation systems.
Cement plants also use stacker reclaimers to manage limestone, coal, and additives for crushing, grinding, and blending processes. Depending on material characteristics and safety requirements, the equipment can also be adapted for other bulk products, including fertilizers and minerals.
Key Factors When Selecting Equipment
Choosing a suitable bucket wheel stacker reclaimer requires careful evaluation of both material properties and site conditions.
Handling capacity is one of the most important parameters. The machine must match the required throughput of the overall material-handling system, including upstream and downstream conveyors.
Stockpile dimensions, rail gauge, traveling distance, boom length, and working range also influence equipment configuration. Material density, particle size, moisture content, and abrasiveness affect bucket design, conveyor selection, drive requirements, and wear protection.
In addition, buyers should consider automation requirements, environmental conditions, existing infrastructure, maintenance accessibility, and compatibility with other equipment. A customized engineering approach can help ensure that the machine meets the specific requirements of each stockyard.
Automation and Maintenance
Automation is becoming increasingly important in modern bulk material handling. Sensors, PLC controls, positioning systems, and monitoring devices can coordinate traveling, slewing, luffing, and reclaiming operations. Intelligent systems using laser scanning and related hardware and software can support stockpile detection, positioning, and automated operation where appropriate.
Regular maintenance is equally important for long-term reliability. Operators should inspect bucket wheels, conveyor belts, bearings, gearboxes, drive units, rail wheels, braking systems, and material-contact components. Electrical equipment, sensors, and safety devices should also be checked according to the manufacturer's maintenance recommendations.
A structured preventive maintenance program can help identify wear and abnormal operating conditions early, reduce unexpected downtime, and improve equipment availability.
Dadi Equipment: Customized Bulk Material Handling Solutions
Jiangyin Dadi Equipment Co., Ltd. specializes in bulk material conveying equipment and high-end metallurgical equipment. Established in 2001, the company offers a range of products, including bucket wheel stacker reclaimers, scraper reclaimers, cantilever stackers, and tripper carriages.
Its services cover project consultation, engineering design, manufacturing, installation, commissioning, operator training, after-sales support, spare parts, and equipment upgrading. This integrated approach helps customers coordinate equipment design with actual stockyard layouts and production requirements.
Dadi Equipment provides customized solutions based on factors such as handling capacity, material properties, stockpile dimensions, conveyor arrangements, structural configuration, and automation needs. Its experience serving customers in more than 30 countries supports applications across metallurgy, mining, power generation, ports, cement, and other bulk material industries.
For more information about its equipment and engineering capabilities, visit the official website: https://en.cndadiem.com/reclaiming-equipment/Bucket-Wheel-Stacker-Reclaimer.html
Conclusion
A bucket wheel stacker reclaimer plays a vital role in modern bulk material handling by combining efficient stacking, continuous reclaiming, and coordinated material transportation in one integrated system. Its performance depends on appropriate equipment selection, reliable mechanical components, effective conveyor integration, and suitable control technology.
For facilities handling iron ore, coal, limestone, pellets, coke, and other bulk materials, a properly engineered stacker reclaimer can support organized stockyard management and a reliable supply of materials to downstream processes.
Working with an experienced manufacturer such as Jiangyin Dadi Equipment Co., Ltd. can help businesses develop customized solutions that meet their operational requirements and site conditions. By considering the complete material-handling process, companies can build a more efficient, dependable, and sustainable stockyard operation.
Related products
-
 Add to cart
Morbi mattis ipsum sem, in gravida dolor venenatis vestibulum. Aenean laoreet, nisi in bibendum dictum, purus libero accumsan enim, id vehicula enim metus vitae ipsum. Maecenas nulla est, dictum quis augue ultrices, dictum rutrum enim. Aliquam erat volutpat.
-
Quisque mi est, blandit sed maximus
Original price was: 63.00$.57.00$Current price is: 57.00$.Add to cartDuis feugiat sapien et augue dignissim porta. Nullam magna velit, laoreet porta vestibulum nec, auctor sed dui. Integer ac sodales enim. Quisque magna est, mollis euismod nibh in, elementum congue orci. Cras viverra, elit vitae iaculis efficitur, turpis urna sodales eros, vel finibus lacus elit sit amet dolor. Praesent at erat in purus pretium laoreet.
-
Fusce congue cursus metus
Original price was: 88.00$.80.00$Current price is: 80.00$.Add to cartNulla feugiat felis tempor sem finibus egestas. Maecenas est nunc, faucibus in tristique nec, ornare et tortor. Mauris maximus lectus vel metus finibus, eget ullamcorper leo auctor. Donec at interdum nibh, in blandit massa. Nam pulvinar mollis quam
-
Morbi varius ligula eget ante
Original price was: 55.00$.45.00$Current price is: 45.00$.Add to cartMaecenas nulla est, dictum quis augue ultrices, dictum rutrum enim. Aliquam erat volutpat. Quisque ultricies ornare lacus, eu sagittis urna euismod ac. Nulla rhoncus ultrices ligula, id maximus ligula ultricies non.
-
Nunc tempus facilisis
87.00$Add to cartFusce ullamcorper dapibus eleifend. Nullam ornare pulvinar lacinia. Nunc tempus facilisis ullamcorper. Nam sit amet suscipit risus, ut ultricies felis. Vivamus a finibus nisi. Sed quam sem, accumsan eget tristique sit amet, suscipit sit amet augue. Duis dolor dui, sagittis at faucibus ac, varius et sapien.
Reviews
There are no reviews yet.